If you’ve ever wandered around a machine shop long enough, you’ll notice one thing that separates a smooth-running CNC job from a chaotic, parts-damaging headache: no one likes staring at a pool of shavings and coolant slop on the floor next to a vertical machining center (VMC). That’s where the chip removal system comes in—and if you’re buying a VMC from us, this part isn’t an afterthought we just throw in to check a box. It’s one of the biggest unsung heroes that keeps your spindle running true, your tool life long, and your operators coming back the next day instead of grumbling about cleanup at the end of their shift. Vertical Machining Center
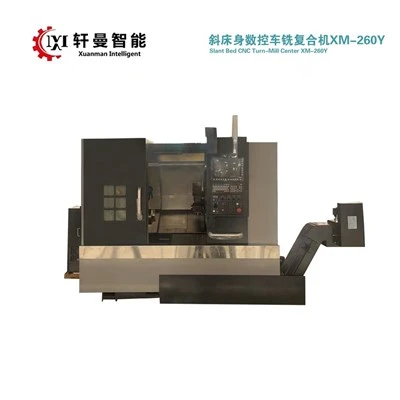
Let’s break this down like we’re talking shop floor over a cold coffee, no fancy engineering jargon that makes your eyes glaze over. First off, a vertical machining center is exactly what it sounds like: the spindle hangs straight down, cuts parts clamped on a table that moves along X, Y, and Z axes. When that drill, end mill, or tap bites into a block of aluminum, steel, or even a composite, it doesn’t just cut away material—it chews it into chips. Those chips? If you let them pile up, they get dragged back into the spindle’s bearings, scratch the part you’re working on, and clog the coolant lines that keep the tool from overheating. That’s not a “minor inconvenience”—that’s a $1,000 part ruined and a VMC down for two hours while you tear it apart to fix the mess.
So what is a VMC chip removal system, really? At its core, it’s a set of parts and processes designed to pick up those chips before they turn into a problem, move them out of the work zone, and get rid of them so you don’t have to. Most good setups aren’t one single part—they’re a team. Let’s start with the first line of defense: the way the VMC’s table and work envelope are built. On almost every VMC we sell, the work table is angled ever so slightly, like a shallow ramp. Chips are heavy, even small ones, and gravity is on our side here—they slide right off the work area toward the back of the machine, where the main chip conveyor lives. No random pileups under the spindle, no operators kicking shavings around mid-job. It’s simple, it’s cheap, and it works way better than any fancy sensor ever invented.
Next up, the chip conveyor. This is the workhorse of the system, and there are two main types you’ll see on VMCs, depending on what you’re cutting. First is the scraper conveyor, which is what we put on most of our standard models. It’s a chain with flat steel scrapers attached, kind of like a tiny, slow-moving assembly line. As the conveyor runs, those scrapers push chips up a gentle incline and dump them into a bin at the end. Why do we like scraper conveyors? They’re tough—they can handle big, thick chips from steel work, no bending or breaking. They’re also low-maintenance; you don’t have to baby them or replace parts every six months. The other type is a magnetic conveyor, which we recommend mostly for aluminum and other non-ferrous metals? Wait no, wait—magnetic conveyors grab ferrous chips, like steel, using a magnet in the center of the chain. Good for fine shavings that would just scatter or get stuck in a scraper, but they don’t work on aluminum, brass, or plastic chips. We never sell a one-size-fits-all conveyor because we know your shop cuts different stuff. If you make auto parts from steel, scraper is the way to go. If you run a shop making aerospace parts from titanium, you might want a magnetic one to grab those tiny chips before they get lost.
Wait, there’s also the side of the VMC that we don’t always talk about: the coolant system ties right into the chip removal too. When a tool cuts, coolant isn’t just there to keep the tool cold—it flushes chips away from the cutting edge and into the chip zone. A lot of cheap VMCs skimp on the coolant pumps, so you get weak flow that only moves half the chips, and the rest get caked on the part or stuck inside the machine. On our VMCs, we spec high-pressure coolant pumps that blast right at the cutting area, so chips don’t have a chance to stick. And we add a mesh filter in the coolant tank that catches any small chips that slip past the conveyor, so they don’t recirculate and scratch the next part you run.
Let’s get real for a second—we’ve seen shops buy the cheapest VMC they can find, then end up spending three times as much on fixing chip-related problems a year later. Spindle damage from chips getting into the head, ruined parts from scratched surfaces, operators taking an extra hour at the end of every shift to sweep and pull chips out by hand. That’s not a deal, that’s a trap. When you buy a VMC from us, the chip removal system isn’t an add-on you have to pay extra for. It’s built into the design, tested on every single machine before it leaves our facility. We run each machine through a full 8-hour cycle cutting chips, making sure the conveyor runs smooth, the angle is right, no chips get stuck in dead spots.
There’s a common myth out there that chip removal systems are overkill for small jobs. Let’s test that. Say you’re running a 10-part aluminum batch on a VMC, each part taking 20 minutes. If your chip system is bad, half the chips end up stuck in the work zone. You have to pause every 10 parts to pull them out, which adds 30 minutes to your day. Multiply that by 200 batches a year, and that’s 100 hours of lost time—way more than the extra you’d pay for a good chip conveyor. For high-volume shops running 24/7? It’s non-negotiable. We’ve had customers with VMCs running two shifts a day for 5 years straight, and their only chip-related maintenance is emptying the bin once a week. That’s the kind of reliability we stand behind.
Another thing we always emphasize to buyers: easy access for maintenance. A lot of cheap VMCs hide their chip conveyor under a bunch of panels, so if a chip does get stuck, you have to take half the machine apart to get to it. Our VMCs have quick-release panels, so if you need to clear a jam, it’s 2 minutes with a wrench, not 20. We also provide operators with a simple checklist: every shift, check that the conveyor runs, empty the chip bin when it’s full, make sure the coolant level is up. No complicated training, no fancy software updates to remember.
Wait, let’s talk about specific scenarios because that’s what matters. Suppose you’re cutting 4140 steel, which makes thick, curly chips. Those chips are heavy, so a weak conveyor can’t pull them up the incline. We spec our conveyor chain to be rated for 2x the maximum load we expect from that steel, so it never slips or stalls. If you’re cutting 6061 aluminum, which makes thin, flaky chips that can blow around if the coolant is too strong—we tweak the coolant pressure on those machines to flush them without blowing them out of the work zone and onto the floor. We don’t use the same settings for every material, because one size does not fit all when it comes to chips.
We’ve also learned a lot from talking to our customers over the years. One shop owner told us he used to have his operator staying late every Friday to shovel chips out of the machine with a scoop. After he switched to our VMCs with our scraper conveyors, that task went from an hour to 5 minutes of emptying a bin. Another customer makes medical parts, where even a tiny chip left on the part can ruin a $500 raw titanium block. He swears by our magnetic conveyors paired with the mesh filter, because they catch even the tiniest microchips before they can scratch the polished surfaces. Those are the kind of stories that make us proud of our chip systems—they don’t just work, they save our customers time, money, and headaches.
Let’s bust another myth: you don’t need a chip removal system if you have a robot loading parts. Wait, even with robot tending, chips still pile up. If a chip is under the part when the robot clamps it, you get a misload, or a scratched part, and the robot has to stop. The chip system keeps the work zone clean, so the robot can run unattended for longer. We have multiple customers running lights-out shifts with our VMCs, and the chip system is a huge part of that—no one has to come in at 2 a.m. to clear a chip jam because the conveyor didn’t do its job.
So when you’re shopping for a VMC, don’t just look at the spindle speed, the axis travel, or the price tag. Ask about the chip removal system. What type of conveyor is it? Is it sized for the materials you cut? Can you get to it easily if it jams? Is it integrated with the coolant system, or is it an afterthought bolted on the side? A lot of brands will tell you their machine has a chip conveyor, but when you get it, it’s a flimsy one that breaks after 6 months, or it doesn’t move all the chips, or it’s hard to maintain.

At the end of the day, a vertical machining center is only as good as its weakest part, and too many shops overlook the chip removal system like it’s not important. But we don’t see it that way. We design every VMC we sell to run smoothly, for long periods, with as little downtime as possible—and the chip system is front and center in that design. If you’re tired of spending time and money on chip-related headaches, if you want a VMC that keeps your shop running efficiently, let’s chat. We can walk you through our different conveyor options, show you the testing we do, and figure out the right setup for the materials and parts you work with. No pushy sales talk, no hidden fees—just real answers to your real problems.
CNC Drilling Tapping Machine Reference
- Modern Machine Shop. (2021). "Chip Conveyors: The Unsung Heroes of CNC Machining." Cutting Tool Engineering, Vol. 73, No. 5.
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems. Wiley.
- American Machine Tool Distributors’ Association. (2019). Vertical Machining Center Specification Guide. AMTDA Press.
Jiangsu Xuanman Intelligent Equipment Co., Ltd.
As one of the most professional vertical machining center manufacturers in China, we’re featured by quality products and low price. Please rest assured to buy discount vertical machining center made in China here from our factory. Customized orders are welcome.
Address: No.1-1, Weier Road, Jieji Equipment Manufacturing Industrial Park, Sihong County, Suqian City, Jiangsu Province, China
E-mail: jsxmzn@163.com
WebSite: https://www.xm-machs.com/
