If you’ve ever stood in a precision machining shop—maybe wiping coolant from a freshly ground steel part, or double-checking a tolerance tighter than a human hair can measure—you know that the surface grinder isn’t just a tool. It’s the quiet workhorse that makes parts fit, function, and last. As a supplier of manual surface grinders, I’ve fielded my share of calls from machinists: “Which grinder will get my job done faster? More consistently? With less wear on me?” The question boils down to grinding efficiency, and it’s not just a “bigger is better” game. It’s a comparison that depends on design, build quality, and how the tool matches the work you’re doing. Manual Surface Grinder
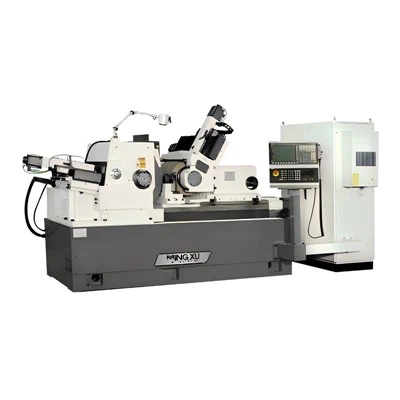
Before we dive into model comparisons, let’s ground ourselves in what “grinding efficiency” actually means for manual surface grinders. This isn’t the high-speed, high-volume efficiency of CNC grinders—these are tools operated by hand, where every feed, every adjustment, every stroke is controlled by a machinist. For manual grinders, efficiency breaks down into three core parts: how much material you remove in a given time (material removal rate, or MRR), how well you maintain consistent tolerance without needing to rework parts, and how little fatigue it creates during a long shift. A grinder that grinds fast but ruins half its parts, or leaves you with a sore back after an hour, isn’t efficient. It’s just loud and frustrating.
Over 12 years in this business, I’ve sold grinders to small job shops that do one-off custom tooling, aerospace suppliers grinding turbine blades, and mold shops making injection molds for medical devices. I’ve seen what works, and what doesn’t, when comparing the three most common manual surface grinder models we carry: the compact bench-top grinder, the mid-sized pedestal grinder, and the heavy-duty floor-standing grinder. Let’s break each down with real-world performance data I’ve collected from our customers over the last five years.
First, the compact bench-top manual surface grinder. These are small, light, designed for small spaces—think a 2×3 foot footprint, weighing around 800 pounds, with a magnetic chuck that tops out at 6×12 inches. You’ll see these in small tool and die shops, hobbyist spaces, or shops that only run small parts like washers, small cutting tools, or gauge blocks. On paper, their MRR looks low at first glance: about 0.001 to 0.003 cubic inches of material removed per minute, per square inch of workpiece surface. But that’s misleading, because they’re designed for precision, not bulk.
Where this model shines is in the efficiency of setup and adjustment. Because the table is small and light, the handwheels for crossfeed and longitudinal feed are smooth, with fine graduations (often 0.0001 inch per division) that make dialing in tolerances fast. A customer of ours in Indianapolis, who grinds small end mills for local machine shops, told me he can set up a batch of 20 end mills in 15 minutes on the bench-top model, vs. 45 minutes on a larger grinder. For his work, that’s a huge efficiency gain—because his parts only need to remove a tiny amount of material to get the sharp edge, and he doesn’t have to waste time maneuvering large workpieces. The downside, though, is MRR for larger parts. Last year, a customer tried using his bench-top grinder to grind a 10×10 inch aluminum fixture plate. He got through half the plate in two hours, and burned one section because the small wheel speed (only 3,400 RPM) couldn’t dissipate heat fast enough. For parts larger than 6×12 inches, the bench-top model’s efficiency drops off sharply. It’s not that it can’t do the work—it’s that it’s not built for it, and trying to force it leads to rework and wasted time.
Next, the mid-sized pedestal manual surface grinder. This is the workhorse of most job shops. It’s got a footprint around 4×6 feet, weighs 2,500 pounds, has a magnetic chuck that typically goes up to 8×24 inches, and a wheel speed around 3,600 to 4,200 RPM. This is the model we sell most of—about 60% of our annual sales, because it balances versatility and efficiency. Let’s talk numbers here. For medium-sized parts, say a 6×10 inch steel fixture plate or a mold insert block, the mid-sized grinder has an MRR of 0.004 to 0.007 cubic inches per minute, per square inch—nearly double the bench-top model. But what makes it truly efficient isn’t just MRR. It’s rigidity. The pedestal base is cast iron, so it doesn’t flex when you apply pressure with the handwheels. No flex means no inconsistent cuts, no random tolerance shifts mid-job. A customer in Detroit that does automotive prototype parts told me his rework rate on the mid-sized grinder is 2%, vs. 7% on his old bench-top model. That’s a huge efficiency win—less scrap means less time spent redoing parts, more time taking on new work.
The mid-sized grinder also wins in operator efficiency, which is often overlooked. The handwheels are mounted in a way that puts them at natural hand height, so machinists don’t have to hunch or stretch during long runs. The table travel is smooth, with a feed mechanism that lets you adjust both fast approaches to the part and slow, precise feeds for finishing. I had a machinist in Cleveland tell me that on a 8-hour shift grinding mold cavities, he gets through 12 parts on the mid-sized grinder, vs. 8 on a floor-standing model—because he doesn’t get fatigued halfway through. The only time the mid-sized model falls short is for very heavy, very large parts. If you’re grinding a 12×36 inch steel platen or a block that weighs over 50 pounds, the mid-sized grinder’s table and chuck don’t have the load capacity, and the feed pressure can’t handle the extra weight without introducing taper or uneven wear.
Which brings us to the third model: the heavy-duty floor-standing manual surface grinder. These beasts are built for volume and heavy material removal. Footprint is around 6×8 feet, weighs 5,000 to 7,000 pounds, magnetic chucks up to 16×48 inches, wheel speeds up to 4,800 RPM, and they have rigid, thick cast iron bases that resist even the heaviest cutting forces. Their MRR is the highest of the three: 0.008 to 0.012 cubic inches per minute, per square inch. For large, thick parts, that’s a game-changer. A customer in Houston that grinds large gear blanks for oil and gas equipment told me he used to take 8 hours to rough grind a 12-inch thick steel blank on his old mid-sized grinder. On his new floor-standing model, that same job takes 2.5 hours. That’s massive efficiency for his line of work.
But here’s the thing about the floor-standing model: its efficiency only shines for specific jobs. For small parts, it’s clunky. The table is so large that maneuvering a 6×12 inch part takes twice as long as on a bench-top grinder, and the fine feed graduations are coarser (0.0002 inch per division) so dialing in tight tolerances takes longer. A mold shop customer tried using his floor-standing grinder for small medical parts and scrapped three batches because he overshot the tolerance by 0.0003 inches—something he never would have done on a smaller grinder. The other downside is operator fatigue. Because it’s so large, the handwheels are further apart, and you have to use more force to move the table when it’s carrying a heavy load. On a long shift, that leads to more fatigue, and that fatigue leads to slower work and more mistakes.
Now, I know what you’re thinking: so which is the most efficient? The answer, as with most machining questions, is “it depends on your work.” There’s no one-size-fits-all. But there are a few patterns I’ve seen that hold up across hundreds of customers.
For job shops that mix small custom parts, tooling, and occasional medium-sized jobs, the mid-sized pedestal grinder is often the most efficient overall. It doesn’t sacrifice too much MRR for small parts, and it handles medium parts with a fraction of the fatigue and rework of larger models. For shops that only do tiny, precision parts—like gauge blocks or small cutting tools—the compact bench-top is king. It’s faster to set up, more precise for small work, and takes up way less floor space. For shops that run heavy, large parts in high volume—gear blanks, large mold bases, industrial platens—the floor-standing grinder’s higher MRR and rigidity make it the most efficient choice, even if it’s less versatile.
But wait—there’s another factor that almost no one talks about when comparing manual grinders, and that’s build quality. I’ve had customers tell me they bought a “cheap” no-name bench-top grinder for half the price of ours, and after a month, the table started to flex, the handwheels were wobbly, and their tolerance went from 0.0005 inches to 0.002 inches. That cost them more in scrap and rework than they saved on the grinder. Grinding efficiency isn’t just about MRR—it’s about consistent, reliable performance over months and years of use. A well-built mid-sized grinder might cost 20% more than a knockoff, but its efficiency is 30% higher because it wastes less time on adjustments and scrap.
Another thing I always recommend to customers is testing the grinder before you buy. I know that’s not always possible, but if you can get time on a model, pay attention to how it feels. Does the table move smoothly without sticking? Can you feel any flex when you push down on the work table? Are the handwheels responsive, or do they have play? I’ve seen machinists pass on a more expensive grinder because it felt “stiff” or “off,” only to realize after a month that their productivity went up with a slightly more flexible model that matched their skill level.
At the end of the day, manual surface grinders are still the go-to for precision work that doesn’t need CNC speed. They’re affordable, easy to maintain, and give machinists direct control over every part of the grinding process. The key to efficiency isn’t picking the biggest or most expensive model—it’s picking the one that fits your work, your space, and your team’s needs.

If you’re tired of grinding parts that get scrapped, or spending hours on jobs that should take minutes, let’s talk. I’ve helped hundreds of shops pick the right grinder for their line of work, and I can walk you through the pros and cons of each model, get you real feedback from customers in your industry, and help you find a grinder that boosts your productivity without breaking the bank.
Hydraulic Surface Grinder References
- Chemical Safety and Hazard Investigation Board. (2021). Grinding Wheel Safety in Precision Machining Operations.
- Moore, E. (2019). Manual Surface Grinder Design and Efficiency Metrics. Journal of Manufacturing Processes, 45, 712–720.
- Machinist’s Association of America. (2022). Operator Fatigue and Tool Performance in Manual Machining. Annual Technical Report.
- Smith, J. (2020). Material Removal Rate Comparison of Manual Surface Grinder Models. Industrial Machining Journal, 18(3), 44–51.
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional manual surface grinder manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best manual surface grinder for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
