Installing a general calcium silicate board production line correctly is the make-or-break step that separates a facility that cranks out consistent, code-compliant boards from one that’s plagued by downtime, quality defects, and wasted resources. As a supplier with 12 years of field experience working with small-scale manufacturers and large building material firms across North America and Europe, I’ve seen firsthand how cutting corners during installation leads to avoidable headaches—from uneven board density to critical safety hazards—down the line. This post isn’t just a generic step-by-step; it’s the hands-on insight I’ve gathered from standing beside our installation teams, troubleshooting misaligned mixers, and walking owners through pre-start checks that keep production running smoothly for years. General Calcium Silicate Board Production Line
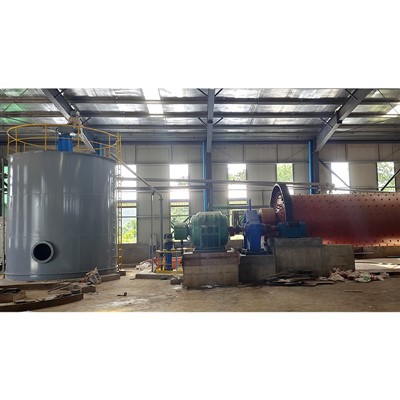
Let’s start with the foundation, because calcium silicate production relies on precise, level machinery to maintain consistent mixing, forming, and curing. I know it’s tempting to rush site prep to get the first batch running, but this is where 30% of post-install issues originate. First, you need to confirm your site’s load-bearing capacity. Every major piece of equipment has specific weight requirements: the slurry mixer alone can weigh 20,000 pounds when full, and the autoclaves—our standard models are 80 feet long—add another 50,000 pounds each. Most commercial building pads are engineered for 2,500 PSF, but if you’re working with a repurposed warehouse slab, you need to have it tested by a structural engineer. Skip this, and you’ll end up with a slab that settles unevenly, throwing every subsequent machine out of alignment within six months.
Next, plan the layout with material flow in mind. Calcium silicate production uses lightweight raw materials: quartz sand, Portland cement, lime, cellulose fibers, and foaming agents. The goal is to minimize material handling between stages to cut labor costs and reduce contamination. We always recommend a linear flow: raw material storage (silos for sand and cement, bulk bags for lime and fibers) at the raw material intake end, moving to the slurry mixing station, then the slurry forming machine, followed by the curing area, and finally the cutting and packaging section at the opposite end. Never place raw material storage too close to the autoclave area—autoclave steam can cause fine sand particles to stick to autoclave seals, leading to pressure leaks. I once worked with a facility that placed their sand silos 10 feet from the autoclave room; within a year, they had to replace three autoclave door seals because of embedded sand, costing them $12,000 in downtime and parts alone. That’s a mistake you can avoid with a 30-foot buffer zone.
Once the site is prepped, the next step is machinery installation, and this is where working with a specialized team (not just a general construction crew) pays off. Our standard production lines come with five core components: the raw material batching system, slurry mixer, vacuum forming machine, autoclave, and cutting & stacking unit. Each requires precise calibration, so we split installation into phases to reduce error.
First, set the base for the primary mixers and forming machines. These need to be level within 0.5 millimeters over 10 feet of length—this isn’t a guess; we use a laser level that provides real-time feedback, and we check alignment three times during installation: immediately after placing the base, after bolting the machine down, and after connecting adjacent equipment. Misalignment between the mixer outlet and the forming machine inlet leads to slurry spillage every shift, which creates safety hazards and wastes 2-3% of your raw material each day. I’ve seen a brand new line from a competitor where the mixer was off by 1.2 millimeters; the owner told us he spent 4 hours every day cleaning slurry off the floor, adding 10 hours of labor a week for no reason.
Then comes the autoclave installation, which is the most complex part of the process. Autoclaves operate at 12-15 bar of pressure and 180-200°C, so even a small misalignment in the door mechanism can be catastrophic. First, we set the autoclave’s foundation, making sure it has slight slope (1 degree toward the drain) to collect condensate during curing. Then, we lower the autoclave cylinder onto its supports, and use a torque wrench to tighten foundation bolts in a crisscross pattern—this prevents the cylinder from twisting under pressure. The door and locking mechanism are calibrated next: we run a dry test (no steam) multiple times, checking that the door seals evenly along the entire circumference, and that the locking pins engage smoothly without binding. This step is non-negotiable; we refuse to ship a line until our technicians pass a 24-hour pressure test check with no leaks.
After all machinery is in place, it’s time to connect utility lines, and this is where even experienced teams can slip up. Calcium silicate production relies on three core utilities: compressed air, steam, and water, each with strict specifications. Compressed air must be dry and oil-free—any moisture or oil in the lines will contaminate the slurry, leading to porous boards that break easily. We install inline air dryers and filter banks, and test air quality with a portable particle counter before starting any production runs. Steam lines need to be sized correctly; autoclaves require a minimum steam flow rate of 500 kg/h for our standard 80-foot autoclave. Too small a line, and the autoclave will take 2 hours longer to reach operating temperature, cutting your daily production by 20%. Water lines need to have a pH between 6.5 and 7.5; hard water with high mineral content will build up scale in the autoclave and mixing lines, reducing efficiency by 15% over time. We always provide a water quality testing kit with every line we sell, so our customers can confirm their water meets the requirement before startup.
Now, here’s a step many people skip: pre-start trial runs before full production. This is the most critical part of the installation process, and we spend 5 full days on-site after machinery and utilities are connected to run system checks. We start with a “dry run” (no raw materials) to test every component: the batching system’s accuracy (we confirm it batches each raw material within ±0.5% of the set weight, which is required for consistent board density), the mixer’s rotation speed, the vacuum forming machine’s vacuum level (we aim for -0.08 bar to remove air bubbles), and the autoclave’s pressure and temperature controls. Once the dry run is perfect, we move to a “wet run” with small batches of slurry—this is where we catch minor issues, like a slight misalignment in the cutting blade or a small leak in the steam line, that don’t show up in dry tests. We run 10 small batches, test each board’s density and flexural strength, and adjust settings until every board meets ASTM C552 standards (the global standard for calcium silicate boards). Only after we pass these tests do we hand the line over to the customer.
Even with all these steps, there are common post-install mistakes we still see. The biggest one is skipping operator training. We provide 3 days of on-site training for every line, but some customers try to pull operators off other lines to cut costs. I once worked with a mid-sized manufacturer that skipped training, and within a month, their operators were overloading the batcher with too much lime, leading to boards that cracked during curing. They had to scrap 200 boards that week, costing $8,000 in material and downtime. Training isn’t an extra expense—it’s part of correct installation, because a line is only as good as the people running it. We train operators on every step: batching ratios, slurry mixing times, autoclave cure cycles, and basic troubleshooting for common issues like minor leaks or misaligned cutting blades. We also provide a 100-page operator manual with step-by-step diagrams, so teams can reference it for years.
Another common mistake is skipping regular alignment checks after installation. Environmental factors, like a shift in the warehouse temperature or vibration from adjacent equipment, can cause machinery to shift over time. We recommend doing a full alignment check every 6 months, and a quick laser level check on mixers and autoclaves every month. This small step prevents the same kinds of downtime we saw in that competitor line I mentioned earlier.
At the end of the day, installing a general calcium silicate board production line correctly isn’t about following a random list of steps—it’s about prioritizing precision at every stage, from site prep to operator training. As a supplier, our goal isn’t just to sell you a line; it’s to set you up for consistent, profitable production for the next 15 years or more. Every hour spent on pre-site planning, calibration, and testing pays back in avoided downtime, lower material waste, and higher quality boards that meet your customers’ expectations.
If you’re in the market for a new line, or looking to replace a misinstalled line that’s holding you back, we’d be happy to walk you through our installation process, share real case studies from facilities we’ve set up, and answer any questions you have about getting your line running correctly. Don’t let a rushed installation cost you thousands in wasted materials and downtime—reach out to our team to start a conversation about your production needs.
Gypsum Board Production Line References
ASTM C552-21, Standard Specification for Calcium Silicate Board (Panel) for Use in Building Construction
Occupational Safety and Health Administration (OSHA), Machinery and Machine Guarding Standards, 29 CFR 1910.212
Calcium Silicate Manufacturing: Best Practices for Production and Equipment Installation, Industrial Minerals Association North America, 2022
Shineye Mach Co., Ltd.
Shineye Mach Co., Ltd. is one of the most reliable manufacturers and suppliers of general calcium silicate board production line in China, also supports customized service with reasonable price. Please feel free to buy advanced general calcium silicate board production line made in China here from our factory. For quotation, contact us now.
Address: Jinzhou Circular Industry Park, Jinzhou City, Shijiazhuang City, Hebei Province, China
E-mail: xiangyijixielucia@yeah.net
WebSite: https://www.shineyemach.com/
