If you’ve ever stood next to a PVC/WPC profile extrusion line during a full production run—chasing a tiny surface scratch on a window frame, troubleshooting a random feed blockage, or watching a whole batch of decking boards get rejected for warping—you know smooth operation isn’t luck. It’s the sum of 100 tiny, consistent moves that most new line operators (or even veteran ones who skip the routine) forget. As someone who’s supplied PVC/WPC extrusion lines for the last 12 years, I’ve seen it all: lines that run 20+ hours a day with 1% downtime, and lines that shut down twice a shift over avoidable headaches. Today, let’s cut the jargon and talk about the real, actionable stuff that keeps your line rolling, no fancy corporate buzzwords required. PVC/WPC Profile/wood-plastic Extrusion Production Line
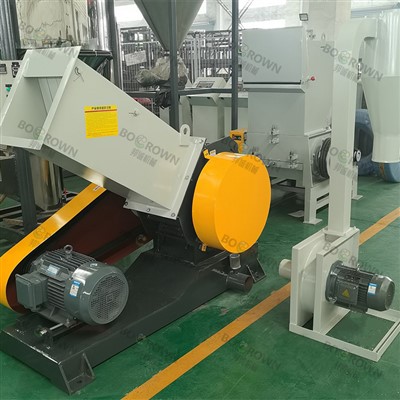
First off, let’s get one thing straight: PVC/WPC is not plain PVC. WPC adds wood flour, right? That’s 30-70% wood by weight, depending on your product—think decking, fence boards, or trim. Wood is way more abrasive than neat PVC, and it’s hygroscopic, meaning it absorbs moisture like a sponge. Mess up the drying step, and you’re looking at bubbles in your profile, surface pinholes, or even extruder screw damage down the line. I can’t tell you how many times I’ve gotten a frantic call from a customer 3 months in saying their line keeps having voids, and when I show up, the dryer is set to 120°F instead of the 180°F we specified, and the hopper filter is caked with unprocessed wood dust. Drying isn’t a “set it and forget it” task. We always tell clients to run the wood flour at 175-185°F for 4-6 hours, and neat PVC at 150-160°F—mix those wrong, and you’ve got a ticket to Problem City. Also, check the dryer’s desiccant beads every 2 weeks. If they’re pink instead of blue, they’re no longer absorbing moisture, and you’re back to those bubbles. Easy win, most people skip this.
Next up, the extruder. This is the heart of the line, and it’s where most hiccups start. First, the screw speed: don’t just crank it up to hit that production quota without checking the melt temperature. PVC has a narrow processing window—usually 350-385°F. Go over 390°F, and you’ll start getting thermal degradation, which looks like brown streaks or charred bits in your profile. Go under 340°F, and the material is too thick, so it won’t flow right through the die, leading to uneven profiles or torn edges. For WPC, you have to bump the melt temp a little—add 10-15°F to account for the wood, but don’t go over 400°F or you’ll burn the wood, which makes your product smell like sawdust and turns it gray. Another big one: the screw’s clearance. Every 6 months, pull the screw and check the gap between the screw flights and the barrel. Wood flour is super abrasive, so that gap wears down over time. If it gets more than 0.020 inches, the plastic can’t melt evenly, and you’ll get inconsistent pressure at the die. I’ve had clients run their lines for 2 years without checking this, and suddenly the line started having random pressure spikes that broke the gearbox. $8k repair, 3 days of downtime, all because they skipped a 20-minute screw check. Also, don’t forget the feed throat. Wood dust builds up there, especially if you’re running high wood content, and that causes the material to bridge—so no material gets into the barrel, leading to a drop in pressure and a slowdown. A quick blast of compressed air in the feed throat every shift fixes that, no tooling required.
Now the die, which is arguably the most important part for profile quality. The die is what shapes your molten plastic into the final product, so if it’s off, nothing else matters. First, before every production run, especially if you switched materials (like from a fence profile to window trim), you have to heat the die evenly. Most dies have 8-12 heating zones, each controlled by a thermocouple. Set each zone to the same temp as your extruder melt, and wait 45 minutes for it to soak in. Don’t just crank the power and start as soon as the light turns green—you’ll get hot spots that cause uneven flow. Then, after running, when you’re done for the day, clean the die immediately. Leave molten plastic in the die overnight, and it will harden, leaving char that ruins the next run. We recommend using a die cleaning compound (the high-temperature stuff, not the cheap generic) and running it through at the end of a shift, then wiping the die surface with a steel wool pad (the fine grade) while it’s still warm, not hot enough to burn you, but warm enough to soften leftover plastic. Also, once a month, do a full die teardown and inspect the lips. For WPC, the wood dust wears on the die lips faster than neat PVC, so if there’s a nick or a scratch, it will show up on every profile. A quick polish with diamond paste fixes small nicks, no need to send the die out for rework every time. Pro tip: mark your die zones with a sharpie so you know which is which— I’ve seen a new operator mix up Zone 3 and Zone 7, leading to a $2k scrap batch because of uneven flow.
Then comes the calibration tank, the part that cools the profile and locks in its shape. This is where a lot of operators cut corners. First, vacuum pressure is key here. Too low, and the profile will warp or get a bad surface finish; too high, and you’ll crush the profile walls. For most WPC decking, we run vacuum at 12-15 PSI, but that changes if you’re running a thin trim profile—crank it up to 15-18 PSI for that. The tank’s water temp is another big one. It should be graduated, right? The first section of the tank, closest to the die, should be the warmest—120-140°F for WPC, not cold water. Cold water hitting hot molten plastic will cause it to cool too fast, leading to internal stress that makes the profile crack later. The last section of the tank should be 60-80°F, so the profile is fully cooled by the time it hits the puller. Also, clean the vacuum screens in the calibration tank every week. Wood dust and plastic buildup clogs the screens, which drops vacuum pressure without you noticing, leading to slow, subtle warping that you might not spot until you stack the boards and see a gap between them. I’ve had a client blame their puller for warping boards, when it was just a clogged vacuum screen—took 10 minutes to clean, fixed the whole problem.
The puller and saw are next. The puller’s job is to pull the profile through the line at a consistent speed. If it’s slipping, the profile will stretch unevenly, leading to dimensional issues. Check the puller’s rubber grips every 2 weeks. If they’re worn down, they’ll slip, especially with WPC which can be a little stickier than neat PVC. A quick wipe of the grips with isopropyl alcohol (to get rid of plastic residue) and adjusting the tension bolts so they’re just tight enough to not slip, but not so tight that they dent the profile, goes a long way. Then the saw: you want a sharp blade, obviously, but for profile cutting, it’s not just sharp—it’s aligned. If the saw blade is tilted, you’ll get angled cuts, which is a huge headache if you’re cutting decking to length for installation (contractors hate crooked ends). Every time you change the saw blade, do a quick check with a square to make sure it’s perpendicular to the profile line. Also, blow sawdust off the cut surface every time—if sawdust gets packed into the cut, it will scratch the profile’s finish.
Don’t forget the upstream and downstream support, because that’s the stuff that’s easy to overlook. Upstream: your material mixing. If you’re not mixing PVC, wood flour, and additives evenly, you’ll get streaks in the profile or inconsistent strength. Use a high-speed mixer, and don’t skip the cooling step after mixing—hot material will start to degrade before it even hits the extruder. Downstream: the conveyor and stacker. If the conveyor is wobbly, or the stacker is dropping boards too hard, you’ll get dents, scratches, or broken profiles. Most small operators don’t invest in automation here, which is fine, but just make sure the line is level. If the conveyor is tilted, heavy WPC boards will slide and get damaged. We always tell clients to use a spirit level on the calibration tank, puller, and saw every month—even a 1-degree tilt can cause problems over a 12-foot profile.
Now, routine maintenance is not a chore—it’s how you avoid unplanned downtime. I’ve seen clients run a line for 5 years with no major repairs, just because they stuck to a consistent schedule. Let’s break it down: daily, weekly, monthly, quarterly, annual. Daily: check all heating zones, make sure melt temp is on spec, check feed throat for bridging, clean vacuum screens, wipe down die. Weekly: check screw clearance (quick peek with a gauge), clean puller grips, calibrate the saw. Monthly: full die teardown and polish if needed, check gearbox oil levels, replace dryer desiccant. Quarterly: inspect extruder feed screw for wear, check calibration tank water temp uniformity, test vacuum pressure. Annual: do a full line alignment, replace worn bearings on the puller and saw, get a professional to calibrate the thermocouples (they drift over time, and wrong temp readings are a huge source of problems). Also, keep a maintenance log—write down every time you check something, every repair you do, every scrap batch you have. If you have a problem, you can look back and see when it started, what changed that day, and fix it faster. No more guessing why the line is acting up.
Wait, and one more big thing: operator training. I can give you the best line, the best die, the best maintenance schedule, but if your operator is new and doesn’t know what a normal pressure reading looks like, they’ll shut down the line for no reason, or run it so fast that it breaks. Most new operators only get a day or two of training, which is crazy. When we sell a line, we give 2 weeks of on-site training, not just a manual. We walk through every part of the line, show them what normal is (so they notice when something is off), how to troubleshoot common issues (like bridging, pressure spikes, warping), and how to do routine maintenance. We also have a 24/7 support line—if you have a problem at 2 a.m., you can call us, and we’ll walk you through it, no nonsense. I’ve had clients say training is a waste of money, but 9 times out of 10, the lines that run the smoothest are the ones where the operator actually knows what they’re doing.
Let me wrap this up: smooth operation of a PVC/WPC extrusion line isn’t about buying the most expensive equipment. It’s about small, consistent habits: drying your materials right, checking your die and vacuum weekly, training your operator, and sticking to a maintenance schedule. Skip the desiccant check, and you get bubbles. Skip the die clean, and you get char. Skip the operator training, and you get half the line’s downtime.
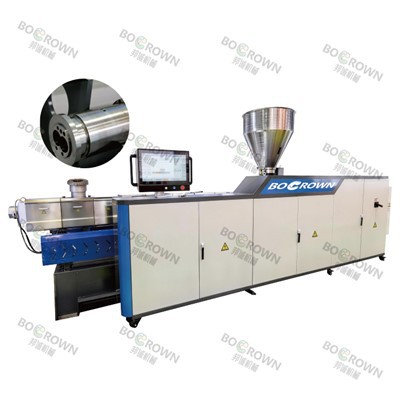
If you’re looking to upgrade your current line, or invest in a new PVC/WPC extrusion line, we’ve helped 200+ small to medium manufacturers get their lines running at max efficiency, with downtime under 2% a year. We don’t do one-size-fits-all—we work with you, whether you’re making decking, window trim, fencing, or something else, to customize the line to your products. If you have questions, want to talk specs, or need help troubleshooting a current line, just reach out. We’re here to help you keep your line rolling, no headaches.
Feeding System References
- Hensen, F. (2019). Extrusion Technology for Wood-Plastic Composites. Hanser Publications.
- Léo, P. (2021). Practical Guide to PVC Profile Extrusion: Maintenance and Troubleshooting. Polymer Engineering Series.
- American Plastics Council. (2020). Processing Guidelines for PVC/WPC Extrusion Lines. Industry Technical Report.
- Zhang, Y. (2018). Wear and Maintenance of Extrusion Components for Abrasive Filled Polymers. Journal of Polymer Processing and Technology.
- European Plastics Converters Association. (2022). Best Practices for Calibration and Pulling Systems in Profile Extrusion. Operational Guideline.
ZJG BC Machinery Co., Ltd.
As one of the most professional pvc/wpc profile/wood-plastic extrusion production line manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy cost-efficient pvc/wpc profile/wood-plastic extrusion production line for sale here from our factory. Contact us for custom service and OEM service.
Address: No.8 Lexi Road, Leyu Town, Zhangjiagang City
E-mail: sales@bcextruder.com
WebSite: https://www.bcextruder.com/
